What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
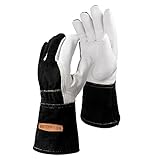
The best tig welding gloves balance 0.6mm to 0.9mm top-grain leather in the palm with an unlined or lightly lined design, shirred or straight seams away from the fingertips, and a 4 to 5-inch cuff for most TIG work. For maximum torch control choose deerskin or kidskin with a short cuff; for mixed TIG and light MIG or stick work, choose goatskin or cowhide with a longer gauntlet.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.



What we cover
What Separates TIG Gloves From MIG and Stick Gloves
TIG gloves are built for dexterity first and heat blocking second. MIG and stick gloves use heavier split cowhide, thick insulation, and long cuffs because you hold a hotter gun and face more spatter. TIG gloves use thinner, suppler top-grain leather, minimal insulation, and tighter patterning so you can feed filler rod, roll the TIG torch, and operate a foot pedal or fingertip control without bunching.
The trade-off is thermal protection. A 0.6mm kidskin glove gives you excellent finger feel for 80-150 amp DC TIG on steel and stainless, but it will heat-soak faster if you rest your hand near the arc or handle hot parts. A 0.9mm goatskin or thin cowhide gloves sacrifices a little sensitivity for more abrasion resistance and slower heat transfer.
Key Decision Criteria Compared
1. Leather Type and Thickness
Material determines feel, durability, and heat resistance:
- Kidskin and deerskin: Softest, thinnest (0.6-0.7mm), best dexterity for low-amperage TIG and aluminum work where you need to feel the filler. Less abrasion resistant and wears faster at the thumb crotch.
- Goatskin: The most common all-around choice. Slightly stronger than deerskin at 0.7-0.9mm, good oil and abrasion resistance, still very tactile. Works well from 20 to 200 amps.
- Top-grain cowhide: Thickest of the TIG-appropriate leathers at 0.9-1.1mm, more heat resistance and longevity, but stiffer until broken in. Better if you switch between TIG, MIG, and grinding.
- Pigskin: Naturally oil-resistant and breathable, often with a slightly textured grain. Moderate dexterity, good for sweaty environments.
Lining matters as much as leather. Unlined gloves give the most direct feel but transmit heat quickly. A thin cotton or Kevlar jersey lining adds a fraction of heat delay and sweat absorption with minimal loss of feel. Fleece or wool lining is too bulky for precise TIG work.
2. Cuff Length and Closure
Cuff length is measured from the wrist crease to the end of the gauntlet:
- Short cuff (3-4 inches): Maximum wrist mobility for bench TIG, good with a long-sleeve welding jacket. Less forearm coverage from UV and spatter.
- Standard gauntlet (4.5-5.5 inches): Covers the gap between glove and sleeve, the best compromise for most fabricators.
- Long gauntlet (6-8 inches): Preferred for overhead, high-amperage TIG or if you wear short sleeves, but can interfere with tight work under a chassis or inside a cabinet.
3. Seam Placement and Stitching
Seam construction dictates where the glove will irritate or fail first. Look for:
- Straight vs. shirred back: Shirred (elastic-gathered) backs expand over knuckles for a snugger fit without extra leather bulk.
- Seam location: Top-tier TIG gloves use a wing-thumb design and move the side seam away from the index finger and thumb pinch point where you feed wire. External or rolled seams reduce internal ridges that affect filler control.
- Thread: Kevlar stitching resists burning and fraying far longer than cotton or nylon. Double-stitched critical seams last longer but add slight stiffness.
4. Fit and Dexterity
A proper TIG glove should fit like a snug driving glove, not a loose work glove. Fingers should reach the end without extra material bunching at the tip, and you should be able to pick up a 1/16-inch filler rod and a dime without removing the glove. Leather stretches 5-8% with use, so a slightly snug new glove is ideal. If you are between sizes, size down for kidskin/deerskin and stay true to size for thicker cowhide.
Spec Comparison: Common TIG Glove Types in 2026
The table below summarizes typical specs you will see from established brands like Tillman, Black Stallion, Lincoln Electric, Miller, Weldas, and Revco. Exact numbers vary by model, but these ranges reflect current market offerings.
| Glove Type / Example Style | Palm Leather & Thickness | Lining | Cuff Length | Seam / Stitching | Sizes Available | Approx. Weight Per Pair |
|---|---|---|---|---|---|---|
| Ultra-Thin Kidskin TIG (e.g., Tillman 24C, Revco Ultra) | Kidskin, 0.6-0.7mm | Unlined | 3.5-4 in. | Wing thumb, external Kevlar | S – XL (7 – 11) | 65-85g |
| Goatskin Precision TIG (e.g., Black Stallion 25, Lincoln K2981) | Goatskin, 0.7-0.9mm | Unlined or thin cotton | 4-5 in. | Straight thumb, Kevlar | XS – 2XL (6 – 12) | 80-105g |
| Deerskin Comfort TIG (e.g., Weldas 10-1000) | Deerskin, 0.7-0.8mm | Unlined | 4 in. | Shirred back, Kevlar | S – XL (8 – 11) | 75-95g |
| Goat/Cow Hybrid TIG-MIG (e.g., Miller Goatskin TIG) | Goatskin palm, cowhide back, 0.9-1.0mm | Cotton jersey | 5.5-6 in. | Reinforced thumb, double Kevlar | M – 2XL (8 – 12) | 110-135g |
| Pigskin Utility TIG (e.g., Tillman 850) | Pigskin, 0.8-1.0mm | Fleece-lined cuff only | 6-7 in. | Gunn cut, Kevlar | M – XL (9 – 11) | 120-150g |
Weight and thickness correlate directly with heat delay. In general, every additional 0.1mm of leather adds roughly 2-4 seconds before you feel uncomfortable heat when holding a part at 6 inches from a 120-amp arc, but it also reduces tactile feedback for feeding 0.035-inch filler.
Decision Matrix: Which Glove for Your Situation
| Your Situation | Best Match | Why |
|---|---|---|
| Beginner learning TIG on steel, mostly under 150 amps, bench work | Goatskin 0.8mm, 4.5-in. gauntlet, Kevlar seams | Forgiving durability while learning torch angle, enough feel to learn filler feeding |
| Racing, aerospace, or sanitary stainless where bead appearance is critical | Kidskin or deerskin 0.6-0.7mm, short cuff, unlined | Maximum fingertip sensitivity for walking the cup and dabbing small-diameter filler |
| Frequent high-amperage aluminum (180-250 amps AC) | Goatskin palm with cotton lining, 5-6 in. cuff | Lining delays heat soak from reflected AC heat without a bulky MIG glove |
| One glove for TIG plus occasional MIG, grinding, and handling hot parts | Goat/cow hybrid or pigskin, 5-7 in. cuff | Abrasion and heat resistance outweighs ultra-fine dexterity |
| Hot shop, sweaty hands, long sessions | Pigskin or unlined goatskin, perforated back optional | Better moisture management and less stiffening from sweat salts |
| Small or large hands that never fit off-the-shelf | Brand that offers XS-2XL with wing thumb pattern | Correct finger length is more important than leather type for control |
Sizing and Cost Per Use: A Quick Calculation
Getting size right saves money. A glove that is too large bunches and wears through at the fingertips 30-50% faster.
Sizing: Measure around your dominant hand across the knuckles with a tape measure, excluding the thumb. Match to the brand’s chart: 7 in. = XS, 8 in. = S, 9 in. = M, 10 in. = L, 11 in. = XL, 12 in. = 2XL. Try the filler-rod test: with the glove on, you should be able to roll a 1/16-inch rod between thumb and index finger without the leather catching.
Worked cost per use: A typical goatskin TIG glove in 2026 costs in the general range of $18 to $35 per pair. If you TIG weld three evenings per week and a pair lasts 3 to 6 months before the thumb crotch or index fingertip wears thin, that is roughly 36 to 72 sessions. At $25 per pair / 50 sessions = $0.50 per session. A kidskin glove at a similar price may last only 2 to 4 months under daily use, raising cost per session to $0.65 to $0.90, but many welders keep both: kidskin for critical beads and goatskin for practice and tacking.
Durability and Ownership Realities
TIG gloves do not fail from spatter like MIG gloves; they fail from abrasion, sweat, and heat cycling.
- What wears first: The crotch between thumb and index finger from feeding rod, the tip of the index finger from propping on the workpiece, and the cuff edge from UV. Kevlar thread helps, but leather thinning there is inevitable.
- Common mistakes: Using TIG gloves to handle hot, sharp, or oily parts, grinding in them, or pulling them on with wet hands. The oils and metal dust embed in thin leather and accelerate wear. Keep a separate pair of heavy work gloves for handling and a dedicated TIG pair for welding only.
- Cleaning and storage: Do not soak leather gloves or machine wash them. Brush off dust, wipe with a dry or slightly damp cloth, and air dry away from direct heat. Storing them crumpled in a hot toolbox cooks the leather and shrinks the fit. Hang or lay flat.
- When to replace: Replace if you can see light through thinned leather at the fingertips, if stitching is frayed exposing skin, or if the leather has hardened and cracked. Hardened leather transmits heat much faster and reduces dexterity.
- Break-in: Kidskin and deerskin need almost no break-in; goatskin softens after 1-2 hours; cowhide may need a few sessions. Flexing the fingers and lightly conditioning with a leather balm made for welding gloves can help, but over-oiling reduces grip on the filler.
How to Choose Without Overbuying
For most hobbyists and light fabrication in 2026, a single pair of unlined or lightly lined goatskin TIG gloves with a 4 to 5-inch gauntlet and Kevlar stitching covers 80% of needs. If you do a lot of low-amp detail work or thin-wall tubing, add a second ultra-thin kidskin pair for those joints. If you regularly run over 200 amps or do overhead TIG, step up to a goatskin glove with a light jersey lining and longer cuff.
Ignore marketing that promises both heavy heat protection and ultimate finger feel in one glove. Physics does not allow it. Choose based on where you place your hands, how hot you run, and whether you prioritize bead feel or forearm coverage, and rotate two pairs to extend life.
FAQ
Can I use TIG gloves for MIG or stick welding?
You can for very light, low-spatter MIG at low amps, but the thin leather will degrade quickly from spatter and radiant heat. For regular MIG or stick, use dedicated heavier gloves and switch to TIG gloves only when you need dexterity.
Are TIG finger cots or partial gloves worth it?
Some welders use a TIG glove on the torch hand and a heat-resistant finger cot or thin glove on the filler hand, or a cut-off thumb and index finger for more feel. They improve sensitivity but reduce UV and heat protection. Use with a long sleeve and be cautious on high-amperage AC where reflected heat is intense.
What cuff length is best if I wear a welding jacket?
With a full welding jacket, a 4-inch cuff is enough because the sleeve covers your forearm. Without a jacket, choose 5.5 inches or longer to prevent UV exposure, which can cause sunburn-like skin irritation over long sessions.
How do I know if my gloves are too thick for TIG?
If you cannot feel the filler rod diameter change between 1/16-inch and 3/32-inch, or you have to over-grip the torch to keep it steady, the glove is too thick or too large for precise TIG control.