
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Our Top Picks

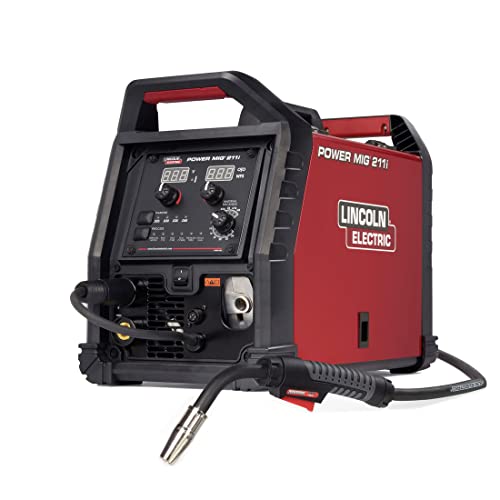
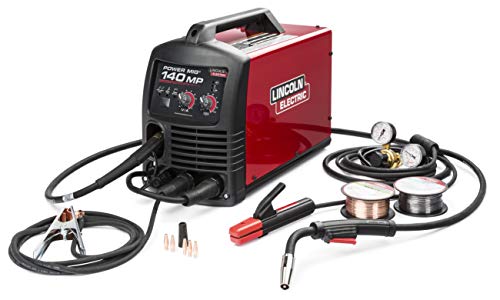

Why galvanized steel changes the job
Galvanized steel is coated with zinc to slow corrosion. In a MIG weld, that coating can contaminate the weld pool, cause extra spatter and porosity, and make it harder to get a clean, consistent bead. Heating zinc also creates hazardous fumes. The welder is only one part of the solution: remove the coating from the weld area, use effective ventilation, and choose a machine that can handle the steel’s thickness and joint type.
For ordinary mild-steel components, a 120-volt MIG welder can be enough for thin sheet and light brackets. For thicker parts, longer welds, or regular shop work, a 240-volt machine gives more usable output and a better duty cycle. Match the machine to the work rather than buying the largest unit available.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.

What to look for in a MIG welder
Check the machine’s rated output, voltage, duty cycle, and wire-feed adjustment. A stated duty cycle of 20% at a given amperage means the machine can weld for two minutes out of a ten-minute period at that output before needing to cool. Ratings only make sense when compared at the same amperage and duty cycle.
For most galvanized mild-steel components, solid ER70S-6 wire with an appropriate shielding gas is a practical choice. A common starting setup for thin steel is 0.023-inch wire; 0.030-inch wire is a useful general-purpose size for heavier material. Follow the welder and wire manufacturers’ charts, then test on scrap of the same thickness. Wire speed, voltage, travel speed, joint fit-up, and shielding gas all affect the result.
Look for a stable feed system, a gun and ground lead that suit the job, and a clear way to adjust voltage and wire speed. Synergic or preset controls can speed setup, but they do not replace test welds. A spool-gun connection is useful if you also plan to weld aluminum, but it adds cost and is not needed for galvanized steel.
Welder types compared
| Machine type | Best fit | Trade-off |
|---|---|---|
| 120V MIG, roughly 90–140A maximum | Thin panels, small repairs, occasional home-shop work | Limited output and shorter duty cycles; may struggle on thicker joints |
| 120/240V dual-voltage MIG, roughly 140–200A maximum | Mixed light work, portable use, and occasional heavier fabrication | Costs more than a basic 120V machine; full output usually requires 240V |
| 240V MIG, roughly 180–250A maximum | Frequent shop use, thicker components, and longer welds | Needs a suitable 240V circuit and is less convenient to move |
| Gasless flux-core-capable MIG | Outdoor work where wind makes shielding gas difficult | More smoke and spatter; flux-core is not automatically the best choice for clean indoor welds |
Which type should you buy?
For occasional repairs on thin galvanized sheet, a basic 120V machine is often the sensible buy. It costs less and is easier to power, provided the material is within its rated capacity and you can work in short runs. Compare 120V MIG welders that support solid wire by checking their published output and duty cycle, not just their maximum amperage.
If you expect to weld a mix of thin and medium-gauge parts, a dual-voltage machine offers more room to grow. It can run from a 120V outlet for light jobs and deliver more output on a properly wired 240V circuit. Consider dual-voltage MIG welders if portability and flexibility justify the extra cost.
For production work or components that routinely exceed a small machine’s comfortable range, choose a 240V unit with a duty cycle suited to your schedule. A higher rating does not guarantee better welds: poor fit-up, contaminated steel, or incorrect settings can still cause lack of fusion and porosity.
Prepare and weld galvanized steel safely
Before welding, identify the coating and remove zinc from both sides of the joint where practical. Grind back to clean steel beyond the weld area, using a suitable abrasive and eye and respiratory protection. Do not assume a quick pass over the visible seam has removed enough coating underneath an overlapping joint. Clean off oil, dirt, and grinding debris as well.
Work outdoors or use local exhaust ventilation positioned to capture fumes without disturbing shielding gas. Avoid putting your face over the weld plume. Zinc-oxide fume can cause metal fume fever, with flu-like symptoms that may appear hours after exposure. If the work cannot be ventilated effectively, stop and arrange appropriate controls and respiratory protection with competent safety guidance. A standard welding helmet is not a substitute for fume control.
Clamp the parts securely and leave a consistent root gap if the joint design calls for one. Tack the assembly to limit movement, then weld with short, controlled passes where heat distortion is a concern. Excessive heat can burn away coating well beyond the seam and warp thin components; too little heat or too fast a travel speed can leave a weak, poorly fused joint. On scrap, check for even bead shape, fusion at both edges, and excessive spatter. If the part is load-bearing or safety-critical, follow an appropriate qualified welding procedure rather than relying on appearance alone.
Common problems and when to change approach
Porosity often points to zinc or other contamination, poor gas coverage, drafts, or a dirty surface. Spatter can come from unsuitable settings, poor stick-out, or coating contamination. If a weld keeps producing holes despite careful cleaning and setup, stop and reassess the joint and ventilation instead of turning up the voltage blindly.
Flux-core wire can be useful outdoors, where wind can blow away shielding gas. It generally produces more smoke and slag, so it is not a shortcut around zinc removal or fume control. For sheltered indoor work on clean, prepared galvanized steel, solid wire with gas usually offers a cleaner bead and less post-weld cleanup.
After welding, remove slag if using flux-core and inspect the entire joint. Restore corrosion protection on the bare steel with a compatible zinc-rich coating or other specified protective system once the surface is clean and cool. That repair helps protect the exposed area, but it does not make unsafe fume exposure acceptable during welding.
FAQ
Which type should you buy?
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!