
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
E7014 is a good choice when you want a mild-steel fillet weld that lays down smoothly with relatively little effort. Its iron-powder coating supports a higher deposition rate than many general-purpose rods, while the rutile-based arc is typically steady and easy to control. The trade-off is that E7014 is not a low-hydrogen electrode, so it is not the right pick for every structural job or every damp, dirty workpiece.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


What we cover
Our Top Picks
 Lincoln Electric ED033506 Fleetweld 47-RSP Stick3/32" x 14", 5 lb Tube14 x 2.18 x 14.45 inches5 PoundsCheck on Amazon

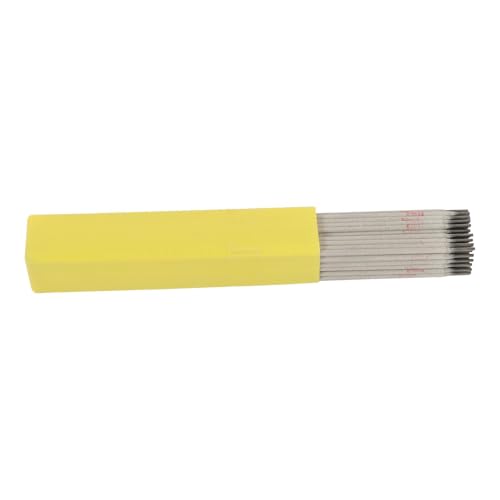

What E7014 is good at
The AWS classification tells you what to expect: “E” means electrode, “70” indicates a minimum tensile strength of 70,000 psi for the deposited weld metal, “1” means all-position classification, and “4” identifies an iron-powder, titania-type coating. Although classified for all positions, E7014 is most comfortable in flat and horizontal fillet welding. Vertical and overhead work take more practice, and the rod’s fluid puddle can make them less forgiving than a suitable low-hydrogen electrode.
For brackets, frames, mower repairs, and general mild-steel fabrication, E7014 can make a wide, even bead with good deposition. It is often a sensible choice when appearance and speed matter more than low-hydrogen properties. For a critical load-bearing connection, follow the drawing or welding procedure: a rod’s strength classification alone does not establish that it is suitable.
Choosing a rod and size
| Rod diameter | Typical current range* | Useful for | Watch for |
|---|---|---|---|
| 3/32 in. | About 70–110 A | Thin stock, smaller machines, controlled short welds | Too much heat can still burn through light sheet |
| 1/8 in. | About 100–150 A | Common fillets on moderate-thickness steel | May be too large for a low-output welder or tight corners |
| 5/32 in. | About 150–200 A | Heavier sections and faster deposition | Requires more output and can overwhelm a small joint |
*Ranges are starting points, not universal settings. Check the electrode package, machine duty cycle, and actual arc behavior. Amperage recommendations vary by manufacturer and polarity.
For an occasional repair or a small home project, a small pack of E7014 stick electrodes is enough to test fit and settings without paying for a bulk carton. A larger pack makes sense if you use the same diameter regularly; rods left exposed to moisture or damaged packaging are a poor bargain.
How to get a smooth fillet
Clean the joint first. Remove paint, oil, heavy rust, and scale at least along the weld path. E7014’s forgiving arc does not make contamination harmless: dirt can cause porosity, poor fusion, or an uneven bead. Fit the pieces tightly where possible, and tack them so the root gap does not open as the joint heats.
Set current within the manufacturer’s range and strike on scrap of similar thickness. The arc should run without frequent sticking, while the puddle remains controllable. Use a short arc and a steady travel speed. For a small fillet, a straight, modest weave or stringer bead is usually easier to manage than a wide weave. Pause briefly at each edge to avoid undercut, but do not linger so long that the toe becomes excessively convex or the base metal overheats.
Keep the rod angle suited to the joint—roughly 45 degrees into a T-joint, with a slight drag angle along the direction of travel. Watch both toes, not just the bright center of the puddle. A bead that looks smooth on top can still have inadequate fusion at the root. If the bead piles up tall and narrow, increase travel speed slightly or adjust angle and current. If the arc stubs or the bead is cold and rope-like, check polarity and lead connections, then raise current in small steps.
Common problems and trade-offs
Spatter and slag: E7014 generally runs smoothly, but excessive spatter can indicate wrong polarity, poor ground contact, or settings outside the rod’s range. Let the slag cool enough to release, then remove it between passes. Slag trapped at a toe or between passes can create an inclusion; inspect and clean before covering it.
Porosity: Pores can result from contamination, a long arc, damp electrodes, or drafts. Keep rods dry according to the manufacturer’s instructions; do not assume that baking a general-purpose electrode is appropriate. If porosity persists, stop and check preparation and storage rather than burying it under another pass.
Thin material: A 3/32-inch rod is easier to control than a larger one on light stock, but E7014 still deposits metal quickly. Use short weld segments and allow cooling between them. For very thin sheet, a smaller rod designed for the work or a different process may be easier.
Position and job requirements: E7014’s fluid puddle can sag in vertical or overhead welding. For those positions, or where a specified low-hydrogen procedure is required, choose the electrode called for by the job rather than forcing E7014 to fit. A low-hydrogen E7018 electrode may suit some applications, but it requires proper storage and handling and is not a drop-in substitute for every procedure.
What to buy
For routine mild-steel fillets in the flat or horizontal position, start with E7014 in 3/32 or 1/8 inch, matched to your machine and stock thickness. Buy from a seller that lists the classification, diameter, and package condition clearly. A known brand is useful when you need consistent arc behavior across a box, but paying more is less important than getting the correct rod, keeping it dry, and setting it properly.
If you are unsure, buy a small quantity and make test fillets on scrap of the same thickness before welding the actual part. Cut or break a sample if the joint’s integrity matters; a neat surface bead does not prove adequate penetration. For safety, wear a correctly rated helmet, gloves, and flame-resistant clothing, and keep the work area clear of combustibles.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!