
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Our Top Picks

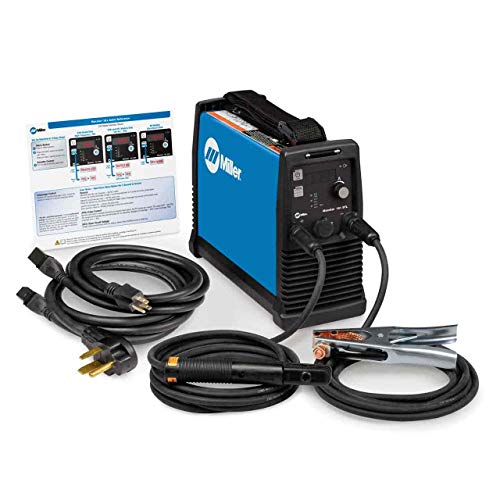

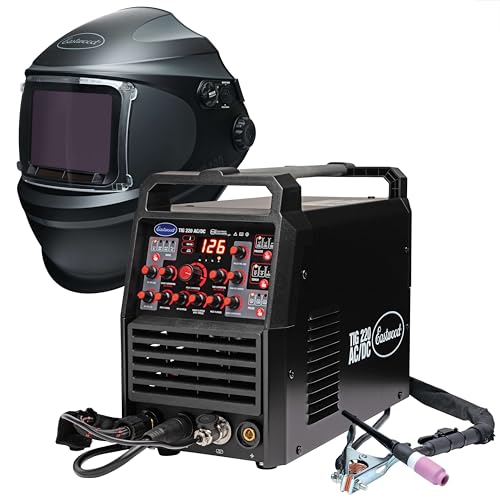
Choosing the right process
For thin stainless steel food containers, TIG is usually the better process. It gives you precise heat control, a small arc, and clean welds with little spatter. That matters when welding 0.5–1.2 mm stainless sheet, where a small amount of excess heat can burn through a wall or pull a lid out of shape.
MIG can still be the practical choice for larger containers, brackets, frames, and production work. It is faster and easier to learn, especially if the parts are not highly visible. A modern inverter MIG welder with short-circuit or pulse settings can weld thin stainless acceptably, but it demands careful setup. Conventional MIG is less forgiving than TIG when joining small, heat-sensitive food-contact parts.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


For a first purchase, a quality AC/DC TIG welder is unnecessary if you only weld stainless; a DC TIG machine is sufficient. Look for adjustable amperage down to roughly 5–10 amps, high-frequency start, post-flow, and a foot pedal or fingertip control.
Why TIG works well on thin stainless
TIG separates the heat source from the filler metal. You can establish a small puddle, add a tiny amount of filler, and stop adding heat immediately when the joint is filled. That control is valuable on seams, corners, and rolled container rims.
For common 304 or 316 stainless, use matching filler such as ER308L for 304 and ER316L for 316. On very thin sheet, 0.8 mm or 1.0 mm filler is often easier to control than thicker rod. You may also autogenously fuse a tight, well-fitted seam without filler, but this leaves less material in the joint and makes poor fit-up more dangerous.
Start around 25–40 amps for 0.6 mm sheet and roughly 40–65 amps for 1.0 mm sheet, then adjust for joint design, tungsten size, and heat sinking. These are starting points, not fixed settings. A 1.6 mm, 2% lanthanated tungsten with a sharpened point works well at low current. Use pure argon at approximately 10–15 cubic feet per hour with a gas lens if drafts or contamination are a problem.
Stainless conducts heat less effectively than mild steel. Heat stays near the weld, causing discoloration and distortion. Use short welds, skip around the assembly, and allow the part to cool. A copper or aluminum backing bar can draw away heat and support the puddle, provided it fits tightly against the work.
When MIG is the better choice
MIG wins on speed. Once the machine is set, you can weld a long seam without stopping to add filler by hand. It is useful for container frames, handles, non-food-contact supports, and repeated assemblies where appearance is less important than throughput.
Use stainless wire matched to the base metal, such as 308L wire for 304 stainless. A common diameter for thin work is 0.6 or 0.8 mm. Use 98% argon/2% carbon dioxide shielding gas rather than a high-CO2 mild-steel mix. Too much carbon dioxide increases spatter, oxidation, and surface contamination. Straight argon is not appropriate for normal MIG short-circuit welding.
A 308L stainless MIG wire is a sensible starting point for 304 containers. Keep the gun close, use a short stickout of about 6–10 mm, and make short tack welds before connecting them. Excessive stickout reduces shielding and makes the arc unstable.
Pulse MIG is easier on thin stainless than standard short-circuit MIG because it can reduce spatter and average heat input. It costs more, however, and does not eliminate the need for clean metal and accurate fit-up. If you only weld a few containers, TIG may be cheaper overall than buying a pulse-capable machine and troubleshooting inconsistent welds.
TIG versus MIG for thin stainless containers
| Factor | TIG | MIG |
|---|---|---|
| Thin-sheet control | Excellent at low amperage | Acceptable with careful settings; pulse helps |
| Typical appearance | Clean, narrow, low-spatter bead | Faster but more visible spatter and profile |
| Learning curve | Steeper; both hands and often a pedal are used | Easier to start and maintain |
| Speed | Slow | Fast |
| Best use | Sealed seams, rims, corners, visible food-contact joints | Long seams, supports, production work, less visible joints |
| Main failure | Burn-through from dwelling or excessive amperage | Spatter, lack of fusion, and distortion from poor settings |
Preparation and welding technique
Cleanliness is not optional. Remove oil, adhesive, paint, and marker residue with a degreaser, then wipe with acetone or an appropriate stainless-safe solvent. Use dedicated stainless brushes and abrasive pads. Tools previously used on carbon steel can embed iron particles that later rust on the container.
Fit the sheets tightly. A gap of even 0.5 mm can turn a controllable TIG seam into a series of burn-through holes. Shear or cut the edges cleanly, deburr them, and clamp the assembly so it cannot move. Tack every 25–50 mm on a long seam, using small tacks rather than large blobs.
For TIG, use a torch angle of roughly 10–15 degrees and keep the arc short. Move steadily instead of lingering to make a wider bead. Back-purge the inside of a closed container with argon. Without an internal purge, the backside can develop black, sugary oxidation called sugaring. It is rough, weak, and difficult to clean from a food-contact surface.
For MIG, start with short stitch welds and let the work cool between passes. Excessive wire feed speed produces a tall, cold bead; excessive voltage widens the arc and increases burn-through risk. Test on offcuts of the same thickness until the bead wets both edges without a hole or heavy buildup.
Food-contact finish and safety
A weld that looks good is not automatically suitable for food contact. Remove heat tint and oxide with a stainless-compatible mechanical method or an appropriate pickling and passivation process. Chemical pickling products can contain hazardous acids, so follow the product instructions, wear the specified protection, and provide ventilation.
Grind only when necessary. Deep grinding marks can trap residue and create crevices. A smooth, blended TIG weld is usually easier to clean than a rough MIG bead. Inspect the finished container for pinholes by filling it with water and checking for leaks, then clean and passivate the surface before use.
Wear a properly rated welding helmet, gloves, nonflammable clothing, and respiratory protection suited to the task. Stainless welding fumes can contain hazardous chromium compounds. A quality auto-darkening welding helmet and local fume extraction are worthwhile, even for short jobs.
What to buy
Choose TIG if the container itself is the project, the sheet is under about 1 mm, the seams must be clean, or you need reliable control around corners and openings. Choose MIG if you already own a suitable machine, the work is mostly structural, or production speed matters more than the finish. For occasional repairs on inexpensive containers, the cheaper MIG option is fine—provided the joint is not a critical food-contact seam and you can accept extra cleanup.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!