
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Our Top Picks
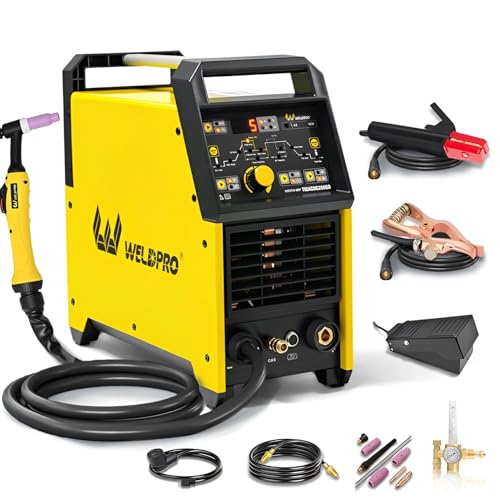 Weldpro 200A AC/DC TIG Welder with Pulse61.8 Pounds17.6 x 7.9 x 16.2 inches61.8 PoundsCheck on Amazon


What separate controls mean
A TIG welder with separate amperage and pulse controls lets you set welding current independently from the pulse parameters. That matters when you want to adjust heat without also changing pulse frequency or the balance between high and low current. On thin stainless, for example, you might lower the peak amps to reduce burn-through while keeping a pulse setting that helps manage the puddle.
Check the control panel before you buy: “pulse” can mean several things. A basic machine may offer only a pulse-on/off switch and one adjustment. More capable units let you set pulse frequency, peak-to-background time balance, and background current separately. Some machines have a dedicated pulse control but only a limited range, so the word “pulse” alone does not tell you how much control you’re getting.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


Why amperage and pulse control matter
Amperage affects how quickly the workpiece heats and how deep the weld penetrates. Pulse alternates between a higher peak current and a lower background current. This can reduce average heat input and help keep a small puddle controlled, especially on thin material or when welding out of position. It does not automatically make a weld stronger or cleaner, and it won’t fix poor fit-up, contamination, or bad torch technique.
For a rough starting point on steel or stainless, many TIG welders work near 1 amp per 0.001 inch of material thickness: about 70 amps for 0.070-inch stock. Treat that as a starting estimate, not a setting rule. Joint type, tungsten size, torch angle, travel speed, and heat sinking all change the result. A foot pedal is valuable because it lets you vary current as you move; a panel setting alone cannot compensate as quickly when a joint gets hotter.
Features worth paying for
For regular thin-material work, look for independent adjustment of peak current, background current, pulse frequency, and pulse time balance. A low pulse-frequency range is useful for visibly timed tacks and learning rhythm; faster settings can produce a steadier arc but may be harder to hear or see. Confirm the machine’s actual adjustment ranges in its manual rather than relying on a product listing that says only “pulse TIG.”
Also check the less glamorous limits. A 120-volt machine may run modest jobs but often has less output and duty cycle than a 240-volt unit. Duty cycle is commonly stated over a 10-minute period: a 40% rating at a given amperage means roughly 4 minutes of welding followed by 6 minutes of cooling under the stated test conditions. Verify whether the welder includes a foot pedal, torch, gas regulator, and consumables; a low-priced bare unit can cost more once those are added.
Comparison by use
| Welder type | Best fit | Main trade-off |
|---|---|---|
| Basic DC TIG with pulse | Steel, stainless, repair work, and occasional thin-gauge jobs | Usually cannot weld aluminum with TIG because it lacks AC output |
| AC/DC TIG with adjustable pulse | Aluminum plus steel and stainless, including varied thicknesses | Costs more and has more settings to learn |
| Simple TIG machine with fixed or limited pulse | Budget work where pulse is an occasional aid | Less control over heat pattern and pulse timing |
If your work is steel only, a capable DC machine can be the sensible buy; paying for AC/DC adds little if you will never weld aluminum. For aluminum, AC/DC is the practical choice. Browse AC/DC TIG welders with adjustable pulse and compare the manual’s control ranges, included accessories, and input requirements rather than choosing by peak amperage alone.
Buy for your work, not the maximum number
Estimate the thickest material you will actually weld, then check the machine’s output at your available voltage. A welder advertised at 200 amps may not deliver that output on a household 120-volt circuit. Check input current, breaker requirements, and the manufacturer’s output chart. If you need to weld 1/4-inch aluminum regularly, a small 120-volt unit is a poor match even if the listing shows a high headline amperage.
For occasional brackets, exhaust parts, or light stainless fabrication, a lower-cost DC machine with a stable arc, usable pedal, and independent pulse adjustment may be enough. Put the savings toward a good helmet, gas lens, and clean filler rod. A gas lens can improve shielding in some setups, but it will not compensate for drafts or a loose gas connection. For aluminum or frequent production work, the extra cost of AC/DC output and a higher duty cycle may be justified.
Common setup problems
Too much amperage can melt a thin edge before you establish a controlled puddle; too little can leave a cold, tall bead with poor fusion. If the tungsten contaminates, stop and regrind it rather than continuing with a dirty tip. A tungsten that is too large can make starting harder at low current, while one that is too small can overheat at higher output. Match it to the current and polarity recommendations for the job.
Pulse settings also have limits. If the pulse rate is high and the background current is too low, the arc may feel unstable or repeatedly lose the puddle. If pulse timing is slow, the bead can show pronounced spacing between peaks. Start with modest pulse settings, make a short test weld on scrap of the same thickness, and change one setting at a time. Keep the work clean, use the correct shielding gas, and check gas coverage before blaming the machine.
A practical shortlist
Choose a DC TIG unit with adjustable pulse for steel and stainless jobs on a budget. Choose AC/DC when aluminum is part of the plan, and favor separate peak, background, frequency, and timing adjustments if you expect to tune heat closely. Compare DC TIG welders with independent pulse controls against the same checklist: power supply, duty cycle, pedal availability, pulse ranges, and service support. Before ordering, download the manual if available. It is the quickest way to confirm that “separate controls” means the adjustments you actually need.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!