
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Our Top Picks
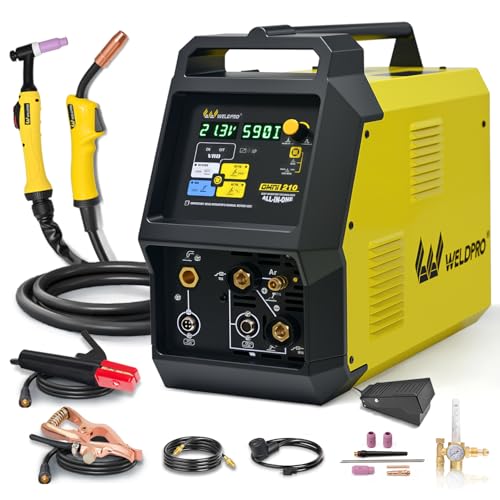 Weldpro Omni210 MIG Welder 200A Multi-Process Welder 110V/220V81.8 Pounds18.4 x 10.4 x 21.1 inches81.8 PoundsCheck on Amazon


What adjustable inductance does
Inductance changes how quickly welding current rises and falls as the MIG welder’s arc repeatedly shorts and re-establishes. In practice, that affects the arc’s feel, spatter, and how the molten pool spreads. Lower inductance generally gives a sharper, more forceful arc; higher inductance tends to soften it and make the puddle wetter. That can change bead profile, but it does not replace correct voltage, wire-feed speed, travel speed, or torch angle.
Manufacturers do not use one shared scale. A dial marked “inductance” may show numbers, a range, or settings such as soft and hard. A higher number on one machine is not necessarily equivalent to a higher number on another. Use the controls to fine-tune a stable setup, then judge the result on scrap of the same thickness and joint type.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


What to buy
For frequent work on steel with short-circuit transfer, prioritize a machine with a genuinely adjustable inductance control, a stable low-amp range, and a wire-feed system that feeds smoothly. A basic 120V MIG welder can be adequate for thin sheet and occasional repairs, but many inexpensive models offer fixed or limited arc tuning. Before buying, check the manual for the adjustment range and whether it applies in the wire-and-gas mode you intend to use.
Compare MIG welders with adjustable inductance if you want to tune short-circuit arc behavior rather than simply choose preset voltage taps. For a home shop, a 120/240V machine is a useful compromise: 120V is convenient for light work, while 240V gives more headroom on thicker material. Confirm the machine’s rated output and duty cycle, not just its maximum amperage. A 20% duty cycle at a stated output means four minutes of welding in a ten-minute period, followed by six minutes of cooling.
Welder types compared
| Type | Best fit | Inductance and trade-offs |
|---|---|---|
| Entry-level 120V MIG | Thin steel, small repairs, occasional use | May have no adjustment or only limited control. Lower cost is reasonable if you can make sound test beads with its fixed arc. |
| Midrange 120/240V MIG | Mixed home-shop work and regular steel fabrication | More likely to offer useful tuning and a broader output range. Costs more and needs suitable 240V power for higher output. |
| Professional inverter MIG | Frequent production work and varied materials | Often provides finer arc control, but added settings and price are wasted if your work is occasional and simple. |
Some multiprocess machines include MIG, TIG, and stick modes, but a long feature list does not guarantee better MIG arc control. Check whether inductance is adjustable in MIG mode, whether the machine supports your preferred wire size, and what accessories are included. A machine that needs a separate spool gun or gas regulator can cost more than its advertised price suggests.
Setting inductance for bead shape
Start with the manufacturer’s voltage and wire-feed chart for your wire diameter, shielding gas, and material thickness. Use clean scrap, keep the stickout consistent—often around 10–15 mm (roughly 3/8–5/8 inch) for common short-circuit setups—and make a short bead at a steady travel speed. Change only one setting at a time.
If the arc sounds harsh, produces excessive spatter, or leaves a narrow, high bead, try increasing inductance in small steps. The pool may become smoother and spread out more. If the arc feels sluggish, the puddle runs too far ahead of the wire, or the weld is excessively flat with poor control on thin material, reduce inductance. The useful setting depends on the complete setup; a broad bead is not automatically a strong bead.
Inspect the finished weld, not only its appearance. For a fillet, check that the weld toes blend into both pieces and that the root is fused. A smooth, wide surface can hide lack of fusion, especially when travel speed is too high or the work is contaminated. If the bead is tall and rope-like, check travel speed, voltage, wire-feed speed, and joint preparation before blaming inductance.
Common failure modes
Too much inductance can make the arc overly soft and the puddle difficult to control; on thin sheet, that may increase burn-through risk if the heat is not managed. Too little can create a hard, spattery arc that makes a rough bead and can make the weld harder to place accurately. Neither adjustment fixes porosity from rust, oil, poor gas coverage, or a leaking hose.
Also check polarity and consumables. Solid MIG wire with shielding gas is commonly used with electrode positive, but verify the wire and machine instructions. A loose drive-roll tension, dirty liner, worn contact tip, or incorrect roll groove can cause uneven feeding that sounds like an arc problem. Drafts can blow shielding gas away; keep the work area protected and use the gas flow recommended for the nozzle and setup rather than turning it up indiscriminately.
When a basic machine is enough
If you weld a few brackets or repair thin steel a few times a year, a lower-cost machine with fixed inductance can be a sensible purchase. Spend the savings on a reliable helmet, suitable gloves, gas, and practice material. Adjustable inductance is most valuable when you regularly tune short-circuit MIG for different joints, wire, and positions—or when a fixed arc makes it difficult to get a controlled bead without excessive spatter.
For heavier work, do not treat inductance as extra welding capacity. Choose a machine whose output, input power, wire-feed system, and duty cycle match the material and production pace. If you want to compare a broader range of shop machines, look at dual-voltage MIG welders with arc-control features and verify the specifications in the manufacturer’s manual before ordering.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!