
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
For vertical-up steel, the best flux-core wire is the one whose classification matches the job, whose diameter suits the material thickness, and whose instructions allow vertical-up welding. For many general-purpose jobs with a gasless wire welder, that means 0.035-inch E71T-11 wire. For thicker plate or structural work, a 0.045-inch E71T-1 wire with the specified shielding gas may be a better fit. Those designations are not interchangeable: check the wire label and your welding procedure before buying.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


What we cover
Our Top Picks
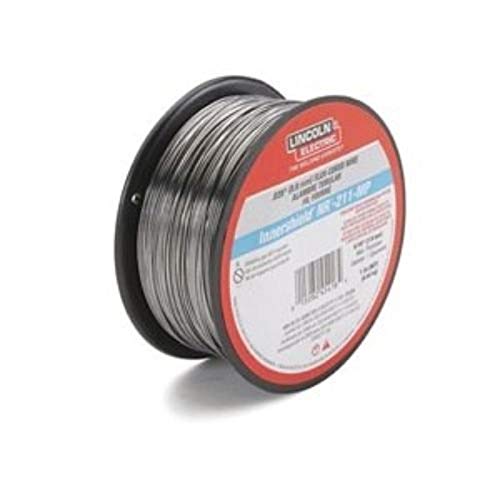 LINCOLN ELECTRIC CO ED031448 .030 NR-2111 Count (Pack of 1)10.5 x 5.75 x 4.25 inches1.15 poundsCheck on Amazon


Choose by job, not by the word “flux-core”
Self-shielded wire makes its own shielding gas from the flux, so it can work outdoors where wind would disrupt shielding gas from a MIG setup. E71T-11 is a common self-shielded choice for general fabrication and is often rated for all positions, including vertical-up. E71T-1 is commonly a gas-shielded wire; its exact position rating and required gas depend on the classification and manufacturer’s data sheet. Do not assume any flux-core spool is suitable for vertical welding.
For light repair and a small 120-volt machine, start by comparing 0.035-inch E71T-11 self-shielded wire with the welder’s manual. It is a practical general-purpose option, not a universal fix: machine duty cycle, output, joint access, and the wire maker’s limits still matter. For thicker steel and a suitable gas-capable machine, consider 0.045-inch E71T-1 gas-shielded wire, but verify the required gas mix, polarity, and position rating first.
Wire options at a glance
| Wire type | Typical use | Vertical-up considerations |
|---|---|---|
| E71T-11, self-shielded | General repairs and fabrication without shielding gas | Often available with an all-position rating; check the spool data. Expect more smoke and slag than solid-wire MIG. |
| E71T-1, gas-shielded | Higher-deposition work on a gas-capable machine | Use only in positions allowed by the specific classification and data sheet. Wind can contaminate the gas shield. |
| Smaller-diameter wire | Thin steel or lower-output welders | Can be easier to control on light material, but check whether the machine can feed it consistently. |
| Larger-diameter wire | Thicker material and machines with adequate output | May deposit metal faster, but can overwhelm a small welder or make a narrow vertical bead harder to manage. |
Wire diameter alone does not determine how thick a plate you can weld. The welder’s output, joint design, number of passes, wire feed stability, and manufacturer’s settings all count. A bigger spool or a higher-strength wire is not automatically a better choice.
How to run a vertical-up bead
Clean the joint to bright metal where possible. Remove paint, oil, heavy rust, and galvanizing near the weld; zinc fumes are hazardous, so galvanized steel needs proper fume controls and appropriate preparation. Fit the pieces tightly and tack them securely. For a butt joint in thicker plate, a bevel and root opening may be necessary; follow the drawing or welding procedure rather than guessing.
Set polarity exactly as specified for the wire. Many self-shielded wires use electrode-negative (DCEN), while many gas-shielded flux-core wires use electrode-positive (DCEP), but the wire’s data sheet is the authority. Using the wrong polarity can cause erratic arc behavior, spatter, poor fusion, or a bead that looks acceptable but lacks strength. Set voltage and wire speed using the manufacturer’s chart, then test on scrap of the same thickness and joint type.
For vertical-up, keep a short, controlled arc and use a small weave or short side-to-side pauses if the joint calls for them. Avoid a wide, slow weave: the puddle can sag, producing an uneven bead or overlap. Watch the leading edge of the puddle, not just the bright arc. If the puddle runs downward, reduce heat or travel more quickly within the wire maker’s recommended range, and use a narrower bead. If the bead sits on top with poor tie-in, check surface cleanliness, travel angle, settings, and fit-up before simply increasing voltage.
Common problems and buying trade-offs
Slag inclusions often come from leaving slag between passes, especially when a weave traps it at the toes. Chip and brush each pass thoroughly before adding another. Porosity can result from contamination, drafts affecting gas-shielded wire, or poor wire storage. Keep wire dry and clean; a rusty or damp spool can feed poorly and make inconsistent welds. Bird-nesting at the feeder points to a feed-path, drive-roll, tension, or contact-tip problem, not necessarily bad wire.
The cheaper spool is fine for occasional repairs if it has a clear classification, intact packaging, and settings your machine can reach. Pay extra for a known manufacturer when you need consistent feeding, reliable batch documentation, or procedure compliance. If a job is load-bearing, regulated, or safety-critical, select wire by the required specification and have the welding procedure and operator qualifications checked; a retail label alone does not establish that a weld is acceptable.
Check these details before ordering
Confirm the machine’s supported wire diameter, spool size, drive-roll groove, contact-tip size, and polarity. Check whether the wire is self-shielded or gas-shielded, and for gas-shielded wire verify the required gas and flow guidance. Compare the wire’s vertical-up rating and recommended settings with the steel thickness and joint you will weld. If you are new to vertical-up, practice on scrap first and inspect the bead for fusion, undercut, overlap, and trapped slag. A steady, well-controlled pass with the right wire is more useful than buying a larger spool before you know the setup works.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!