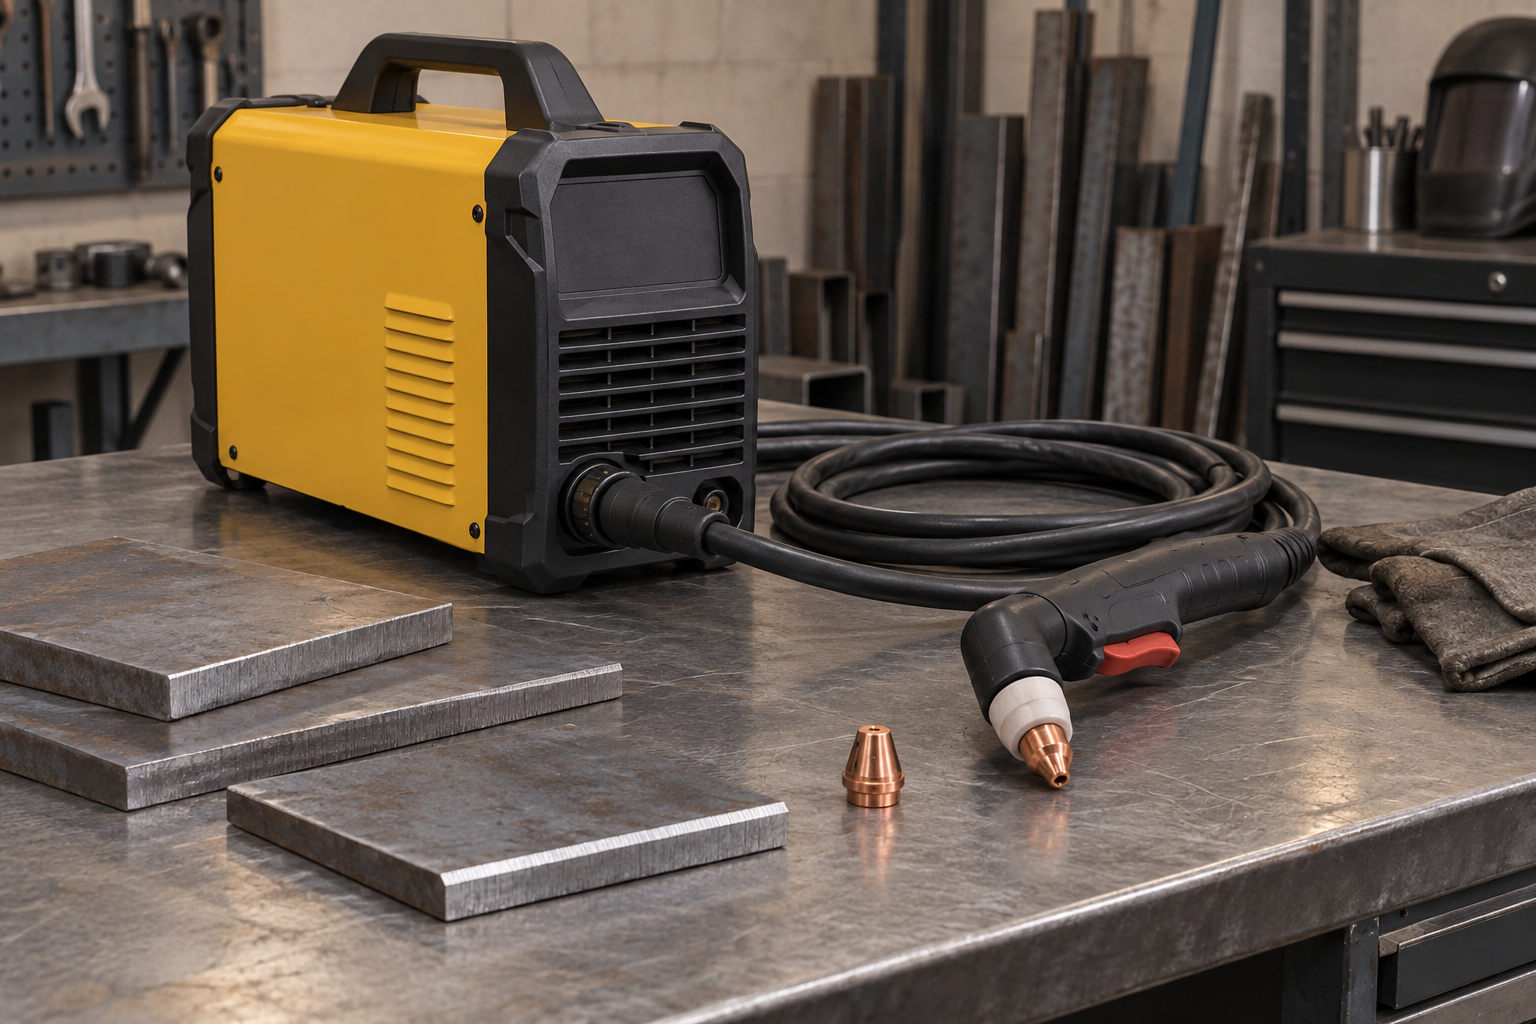
How to Prevent Dross on the Bottom of Plasma-Cut Steel
Dross on the underside of plasma-cut steel is usually a process problem, not a defect in the steel.

1795 articles published
Dross on the underside of plasma-cut steel is usually a process problem, not a defect in the steel.
Square tubing makes clean, strong frames, but it is less forgiving than angle iron or flat bar.
Plasma torch standoff is the distance between the torch tip and the workpiece during cutting or piercing.
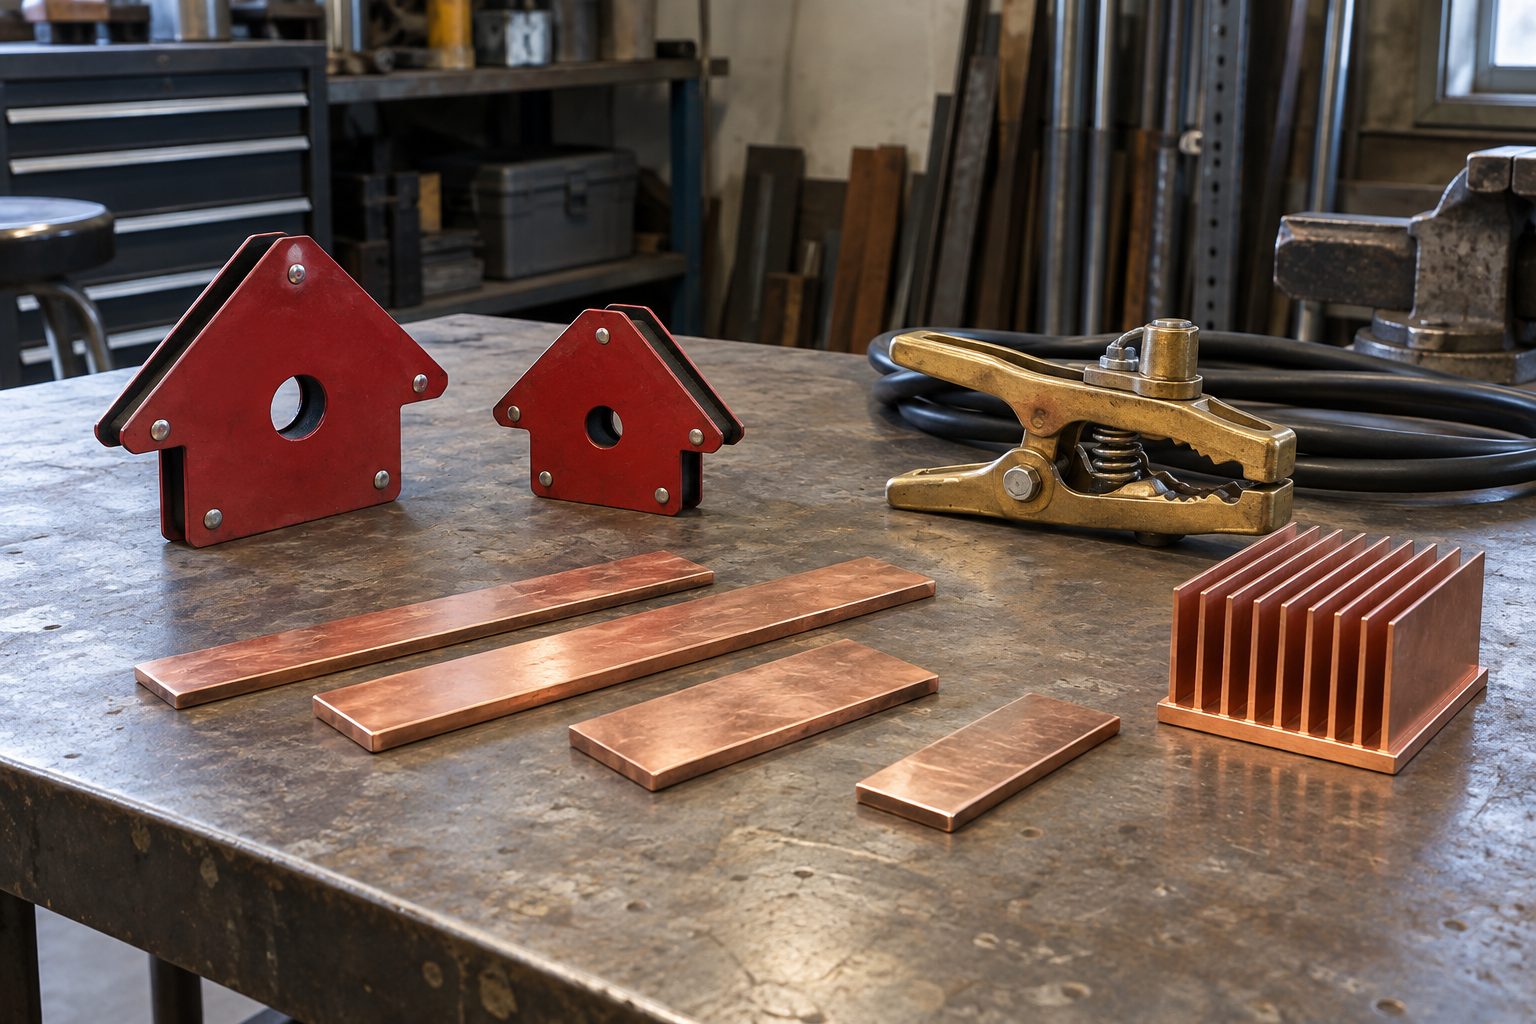
A backing bar gives molten metal somewhere to stop when you weld thin sheet. It reduces burn-through, supports the joint, and helps keep two panels…
Plasma cutter amperage should match the thickness you cut most often, not simply the maximum thickness printed on the box.
Copper backing is a simple way to support a weld on steel, especially when you need a clean root bead on thin sheet or a joint with an open root.
Slag inclusion is trapped nonmetallic material inside a stick-welded joint. It usually comes from incomplete cleaning between passes, an incorrect travel…
Interpass temperature is the temperature of the weld and nearby base metal immediately before you deposit the next pass.
A stick welding rod rarely restarts cleanly by accident. When the arc breaks, the electrode tip is covered with slag and the crater in the weld is usually…
Thick steel removes heat from a weld faster than thin plate. That rapid cooling can produce lack of fusion, porosity, hydrogen cracking, and a hard…