
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Our Top Picks
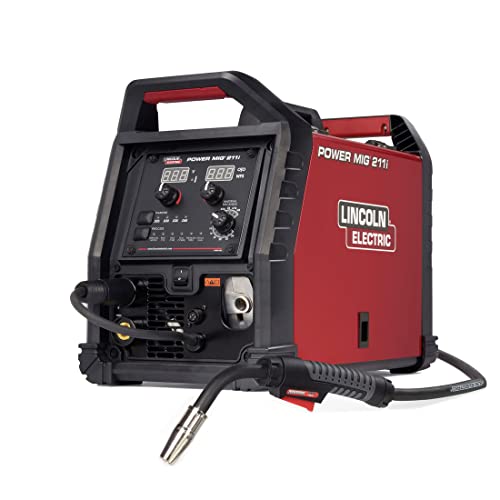
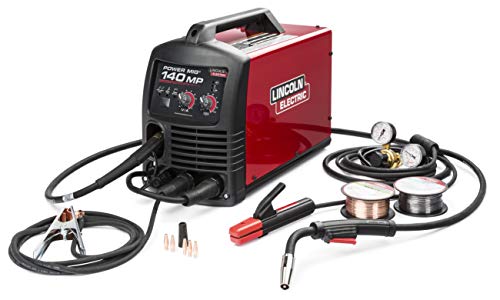


Match the welder to the job
For welding reinforcing bar and flat stock, the right MIG welder depends less on the word “MIG” than on the steel, joint, and location. Flat stock is usually straightforward: a sound machine with a stable low-to-midrange arc can make clean, repeatable fillet and butt welds. Rebar is less predictable. It may be dirty, rusty, oily, or coated, and reinforcing steel is not always intended to be welded. Check the bar grade and project requirements before welding structural reinforcement; some bars need a qualified procedure, and some should not be welded at all.
For shop work on mild-steel stock around 1/8 to 1/4 inch thick, a 120-volt MIG welder can be adequate if you make multiple passes where needed. For regular work on 1/4-inch material, longer welds, or thicker bar, a 240-volt machine gives more useful output and duty cycle. A 180- to 220-amp class welder is a practical range for a small fabrication shop, but check the manufacturer’s rated output and duty cycle rather than relying on the amp number alone.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.

What to look for in a MIG welder
Prioritize input power, a stable arc at low settings, and a duty cycle that fits your work. Duty cycle is the portion of a ten-minute period a welder can run at a stated output without overheating. A rating of 20% at 200 amps means two minutes of welding followed by eight minutes of cooling at that output. Tack-and-fit work may not need much duty cycle; long beads on a bench will expose a marginal machine quickly.
For solid wire and shielding gas, look for a machine that accepts common 0.030- or 0.035-inch wire and has a proper gas solenoid and regulator. Solid wire with 75/25 argon-CO₂ gas usually gives a smoother arc and less spatter on clean flat stock. If the job is outdoors, wind can blow shielding gas away and cause porosity. Flux-core wire avoids the gas bottle, but it makes more smoke and slag and can be less forgiving on thin material. Confirm that the welder supports the flux-core wire type you plan to use.
A 240-volt MIG welder in the 180-amp class is a sensible choice for frequent shop fabrication. A 120-volt MIG welder with flux-core capability costs less and is easier to power, but it is the better fit for lighter, intermittent work than for long, heavy welds.
Quick comparison
| Welder setup | Best fit | Main limitation |
|---|---|---|
| 120 V, solid wire or flux-core | Light flat stock, repairs, occasional tacks | Less headroom and often lower duty cycle |
| 240 V, solid wire with gas | Regular shop work on flat stock and suitable rebar joints | Needs a suitable circuit and gas supply |
| 240 V, self-shielded flux-core | Outdoor work where wind makes gas shielding unreliable | More spatter, smoke, and slag cleanup |
Prepare rebar and flat stock
Preparation often matters more than buying a larger welder. Grind paint, rust, mill scale, oil, and galvanizing away from the weld area and clamp the pieces so the joint cannot shift. Aim for clean metal at least 1/2 inch back from the joint. A weld over contamination can trap porosity or lack fusion; a bead that looks full on top may still be attached only at the surface.
Rebar deserves extra caution. Its ridges make fit-up uneven, while unknown chemistry or high carbon content can make a weld brittle or prone to cracking as it cools. Don’t assume every reinforcing bar is weldable just because it takes an arc. For structural work, follow the project specification and applicable welding procedure, including any preheat and inspection requirements. If those details are unknown, ask the engineer or use a specified mechanical connection instead of improvising.
On nonstructural projects using confirmed weldable steel, a short test weld on matching scrap is worthwhile. Break or cut the sample to check penetration rather than judging only by appearance. If the bead sits high with a cold, rounded edge, increase heat or slow down appropriately; if the base metal burns through or the joint distorts, reduce heat, move faster, or change the fit-up. Let thick joints cool naturally unless the approved procedure says otherwise.
Setup and common failures
Set wire speed and voltage using the machine chart as a starting point, then adjust on scrap of the same thickness. Keep the gun close to the joint and use a steady travel speed. Excessively long stickout can make the arc erratic; too much travel speed can leave a narrow bead with poor fusion. Excess wire speed relative to voltage often produces a harsh, stubbing arc, while too little wire can make the arc burn back toward the contact tip.
Use suitable eye, hand, and body protection, and remove combustible material from the work area. Rebar can roll unexpectedly, so secure it before tacking. Check for coatings before welding: zinc-coated steel can produce hazardous fumes, and removing the coating does not eliminate the need for ventilation and appropriate protection. Avoid welding near sealed containers or unknown residues.
If you need to move between clean flat stock and rougher outdoor work, compare a gas-capable machine with a compatible flux-core option rather than buying solely by maximum amperage. A dual-voltage MIG welder that supports gas and flux-core wire can cover both jobs, though its actual output on a household outlet may be limited. For mostly clean indoor flat stock, spending more for dual voltage or extra modes may not improve the weld. Choose the least expensive machine that has enough rated output, duty cycle, and wire-feed control for the material you will actually join.
Related guides
More from Amazon
Programs that pair well with the guide above. Offers and eligibility are set by Amazon and may change.
A free business account with business pricing and bulk-buying tools for work, shop or home office.
Create a business accountFree shipping on eligible items, Prime Video and more. Eligible new members can start with a free trial.
Start a Prime free trialAudiobooks and podcasts to listen to on the go. Eligible new members can start with a free trial.
Try Audible freeAd-free music streaming. Eligible new subscribers can start with a free trial.
Try Music Unlimited freeAs an Amazon Associate we earn from qualifying purchases.










Write Your Review
No reviews yet. Be the first to share your experience!